High-Performance Woven Bags for Chemicals & Industrial Materials
Our chemical bags are engineered for hazardous powders, resin pellets, and food-grade additives — offering anti-static protection, UN certification, and moisture barrier for global supply chains.
Chemical Bags: Key Applications
Our chemical bags are engineered for a wide spectrum of applications — from commodity materials to hazardous goods.

Industrial Salt

Fertilizer

Pigment

Resin

Rubber

Urea

Chemical Raw Materials

Hazardous Goods
Above are just 8 examples — more applications available
Images for illustration — custom fabric color, weight & width available
Engineered for Chemical Safety & Durability
Our chemical bags are designed to meet the toughest demands of handling, storage, and transport.
Anti-Static / Conductive Options
Built-in conductive yarns or coating to prevent dust explosion risks — ideal for flammable chemical environments.
Moisture & Leakage Barrier
PE lamination or aluminum foil lamination to isolate humidity, oxygen, ensuring chemical stability.
UN Dangerous Goods Certification
Compliant with UN 4G/5H standards, providing hazardous packaging certificate for sea/air export.
High Tensile & Tear Resistance
High denier tapes, safety factor up to 6:1, available from 25kg to 1500kg per bag.
Chemical Bags — Full Technical Specifications
Customizable chemical bags for every application — fabric rolls, woven sacks, valve bags, and more.
📐 Dimensions & Form
- Fabric width: 60cm – 420cm (rolls)
- Bag capacity: 5kg / 25kg / 50kg / bulk
- Roll length: 100m – 1000m
- Gusset: Optional side/bottom gusset
🧵 Material & Strength
- Fabric: Virgin or recycled PP/HDPE
- Density: 6×6 – 14×14 threads/inch
- Weight: 45gsm – 180gsm
- Tensile strength: ≥ 1200 N/5cm
🎨 Additives & Lamination
- UV protection: 2% – 5% masterbatch
- Printing: Up to 8-color gravure/flexo
- Coating: PE lamination, anti-slip, anti-static
- Color: Any custom color (Pantone)
Chemical Bags Trusted by Global Chemical Leaders
Our chemical bags are widely adopted by chemical manufacturers, industrial distributors, and logistics providers worldwide. Whether you need UN-certified bags for hazardous goods, breathable sacks for fertilizers, or durable fabric rolls for industrial covers — our Starlinger production lines ensure consistent quality and reliable performance.
- UN-certified bags for dangerous goods export
- Anti-static & moisture-proof solutions for sensitive chemicals
- Custom printing and lamination for brand and protection
Trusted by Chemical Industry Leaders Worldwide
Decades of experience in woven fabric & bag solutions for chemicals and industrial materials
In-House Production — One-Stop Manufacturing
From yarn extrusion, weaving, coating, to bag conversion — all under one roof. Full traceability and custom development for chemical applications.
Export-Ready & Fully Compliant
Our woven fabrics and bags meet REACH, RoHS, and UN certification standards. Phytosanitary and fumigation-free options available. Supporting your export to global markets.
Need Custom Woven Bags or Fabric for Your Chemical Products?
From UN-certified hazardous goods bags to anti-static packaging and custom-printed woven sacks — our team will tailor the perfect solution for your chemical application. Request free samples and technical data.
Get a Quote →🔬 Recommended Chemical Bags & Products
View all products →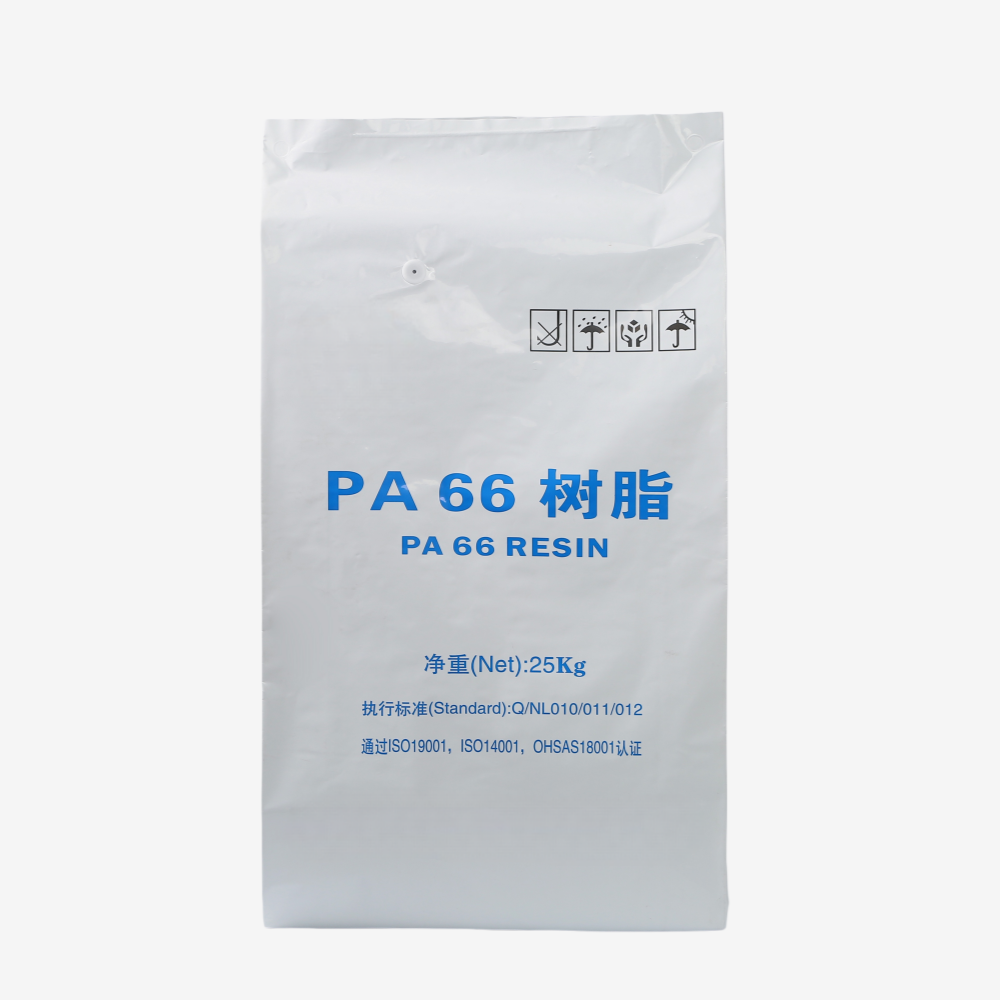
High Barrier Bag
Multi-layer structure with superior oxygen and moisture barrier — ideal for fine chemicals, additives, and humidity-sensitive materials.
Learn more →
PP Woven Sack
Durable, breathable, and customizable — widely used for fertilizer, resin, salt, and rubber.
Learn more →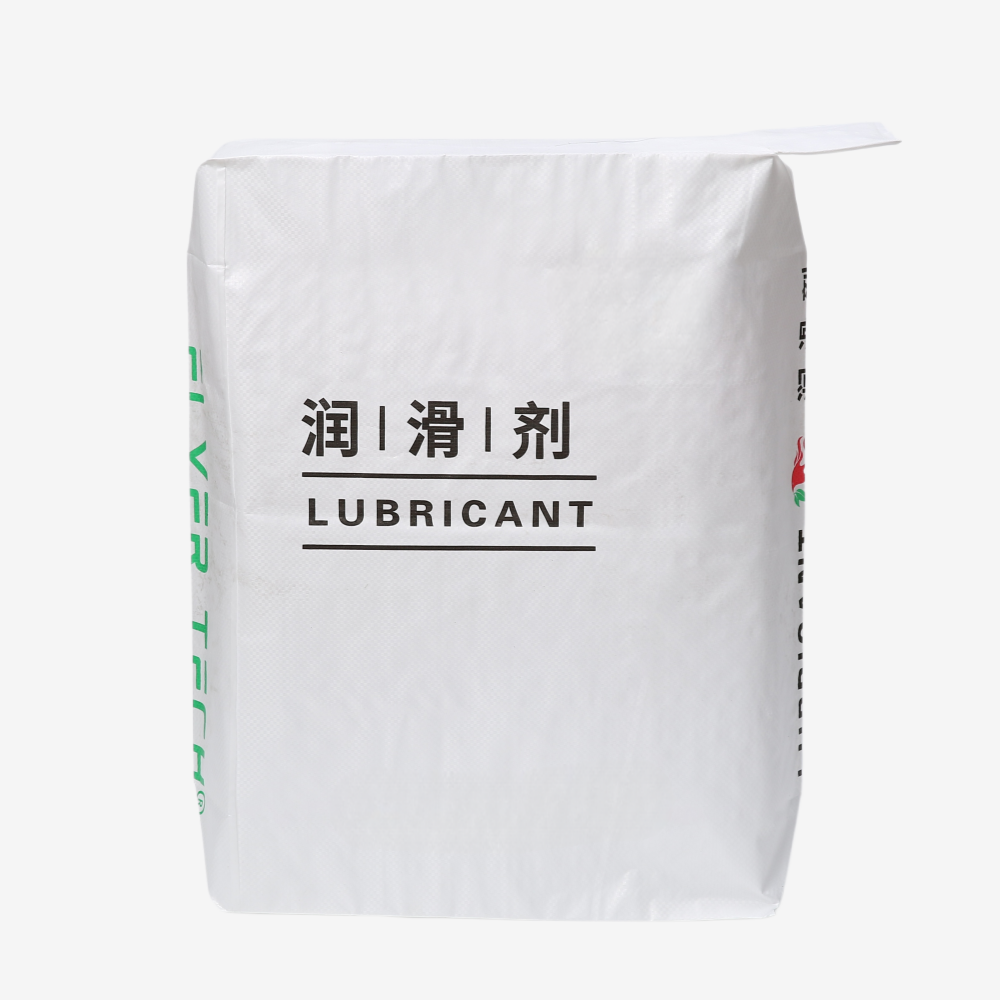
Valve Bag
Designed for powdered chemicals, pigments, and fine materials — dust-free filling and secure closure.
Learn more →